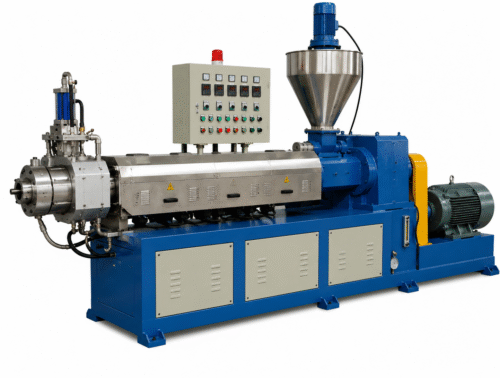
 Rubber Hot Feed Extruder
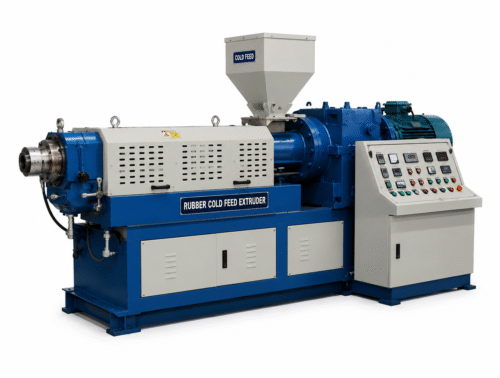 Rubber Cold Feed Extruder
 Rubber Strainer – Reclaim Extruder
 Reclaim Rotary Autoclave
 Compression Molding
 Injection Molding
 Vacuum Molding
 Rubber EVA Refiner Mill
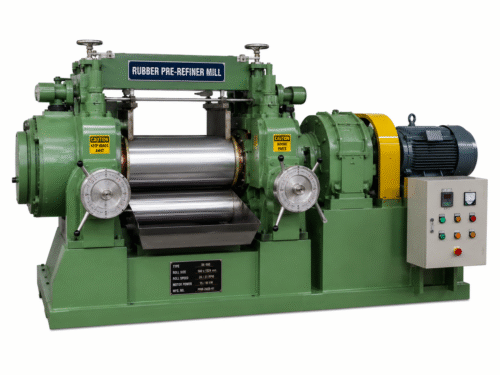 Rubber Pre-Refiner Mill
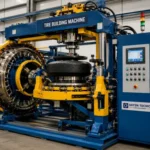 Tire Building Machine
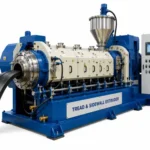 Tread & sidewall Extruder
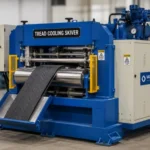 Tread Cooling skiver
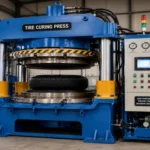 Tire curing press
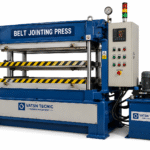 BELT JOINTING PRESS
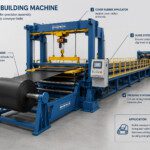 Belt Building Machine
 Eva Footwear Injection Molding Machines
 Hawaii Slipper Sole Sheet Machine
 Eva Sole Sheet Splitting
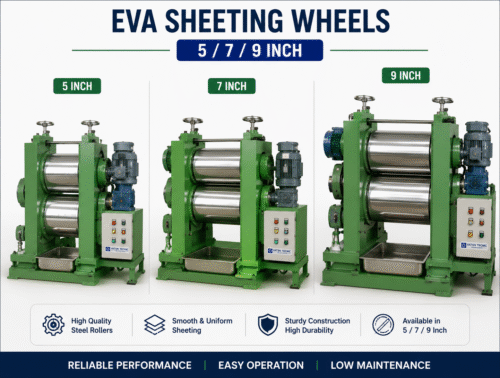 Eva Sheeting Wheels 5/7/9
 PVC Flooring Machine
 Plastic Pelletizing Line
 Filler / Masterbatch / PVC / TPR / EVA
 Breaker – Cracker Mill
 Shredder – Rasper Machines
 Waste Rubber Crumb Grinder Mill
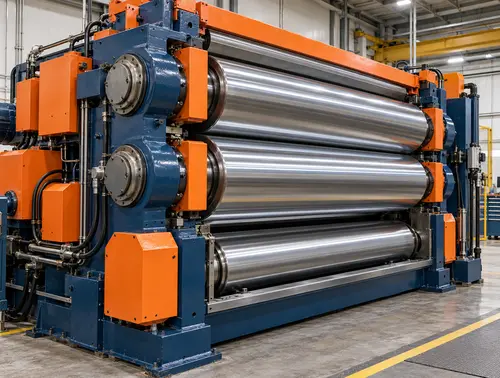
Compare Rubber Calendar Machine in Ludhiana: Cooling and Winding Line

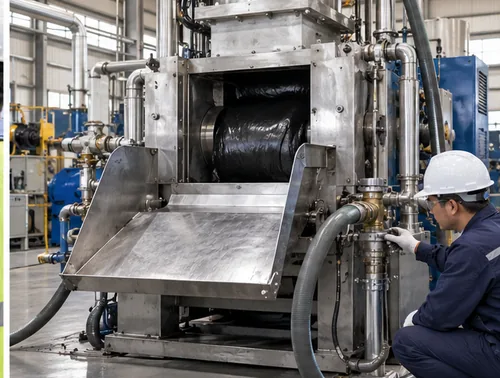
Quick answer: A rubber calendar machine in Ludhiana is only as good as the line after it. If the cooling section is too short, the winding tension is uncontrolled or the edge trim is crude, the sheet that leaves the calender will still be out of tolerance by the time it reaches the pallet.
Buyers spend their attention on the rolls and treat the take-off as an accessory. In practice the cooling distance, the roller spacing and the winder decide whether the sheet is flat, whether the edges are clean and whether the roll can be used without rework. A rubber calendar machine in Ludhiana should be specified as a line, not as a single machine.
This guide covers the take-off decisions that matter, and the questions to settle before the foundation is laid.
Why the take-off line decides sheet quality
Rubber leaves the calender hot and soft. It has to be cooled under control, kept under even tension and wound without trapping air. Each of those steps can introduce a defect that the calender itself cannot fix. A sheet that cools unevenly will curl; a sheet wound under varying tension will deform in storage.
The take-off also sets the achievable line speed. A calender that can run faster than the cooling section can handle is a calender that will always run at the cooling section’s limit.
Cooling sections and roller spacing
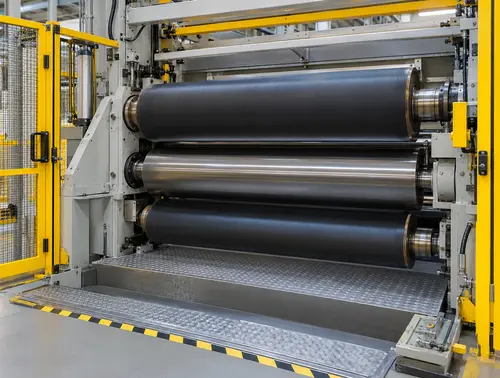
Cooling is usually done over a series of driven rollers in a trough or with air. Water cooling is compact and effective but needs clean water and a drain; air cooling is simpler but takes more space. Whichever is chosen, the sheet must be supported so it does not sag between rollers while still soft.
Winding, tension and edge trim
A winder that pulls harder on one side produces a roll that looks acceptable and behaves badly when unwound. Tension control, a dancer roller or a load cell, and a straight edge trim all contribute. Trim quality matters more than it looks: a ragged edge becomes a crack initiation point when the sheet is later used.
| Cooling method | Strength | Limitation | Best fit |
|---|---|---|---|
| Water trough with driven rollers | Compact, fast cooling, stable sheet path | Needs clean water, drainage and maintenance | Thin sheet, high line speed |
| Air cooling over rollers | No water system, easy to inspect | Longer line, slower cooling | Thicker sheet, moderate speed |
| Drum cooling | Very compact, good surface finish | Drum condition affects both faces | Thin technical sheet |
Layout and floor space in a Ludhiana shed
The distance from the calender to the winder is fixed once the foundation is cast. Measure it against the longest cooling line you might need, not the one you are buying today. Adding two metres later is a civil project; allowing for it now costs nothing.
Access matters as much as length. Operators need to reach both edges of the sheet, and maintenance needs to reach the rollers without climbing over the line. In a crowded shed, the take-off is usually the first thing to be squeezed, and the first to cause trouble.
| Winding option | Strength | Limitation | Best fit |
|---|---|---|---|
| Surface winder | Simple, forgiving, easy to thread | Tension control is indirect | Thicker sheet, short runs |
| Centre winder with tension control | Consistent tension, tighter rolls | Needs a dancer or load cell | Thin sheet, long runs |
| Cut-to-length stacker | Flat sheets, no winding stress | Occupies floor space | Moulded sheet blanks |
Quotation and commissioning
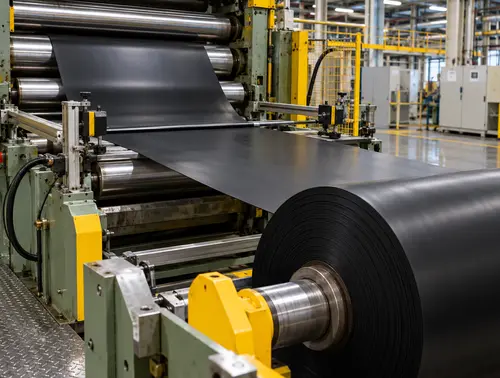
Ask for the take-off as a separate line in the quotation: cooling section, drive, winder, trim and controls. Confirm who supplies the cooling water, who commissions the tension loop and what documentation arrives. A calender sold without a take-off specification is only half a line.
At commissioning, run the sheet at the lowest speed and watch the path through the cooling section. Then increase speed and check that the sheet stays flat and the edges stay clean. Record the tension settings that work, because they will be the starting point for every future product.
For the roll and frame checks that go with the line, see roll crown and grinding history and roll heating circuit handover.
Specifying a calender line? Vatsn Tecnic supplies new, used and refurbished rubber processing machinery. Share your sheet width, thickness and target output, and ask for the take-off scope alongside the calender itself.
To read More about Rubber Making Machine Visit Here:
https://www.indiamart.com/vatsntecnic/profile.html
Frequently asked questions
How long should the cooling section be?
Long enough to bring the sheet down to a temperature where it can be wound without deformation at your target line speed. Calculate it with the supplier rather than copying another plant.
Can I add cooling later?
Yes, but it usually means extending the foundation and re-aligning the line. Allowing the floor space now is far cheaper.
Does the winder affect sheet quality?
Yes. Uneven tension deforms the roll and shows up as waviness when the sheet is unwound. Tension control is not a luxury on thin sheet.
What causes curled edges?
Usually uneven cooling across the width, or a trim that leaves a stressed edge. Check the cooling distribution first.
Is edge trim necessary?
Almost always. The calender produces a slightly thicker, less controlled edge, and trimming gives a clean, consistent width.
What water quality does a trough need?
Clean, cool and free of suspended solids that would mark the sheet or block the spray. Confirm the supply and the drain before installation.
How do I set the line speed?
Start from the cooling capacity, then check the winder and trim can keep up. The slowest element in the line sets the production rate.
What should be in the commissioning record?
Line speeds, cooling water temperature, tension settings and the visual condition of the sheet at each speed. That record becomes the baseline for future products.