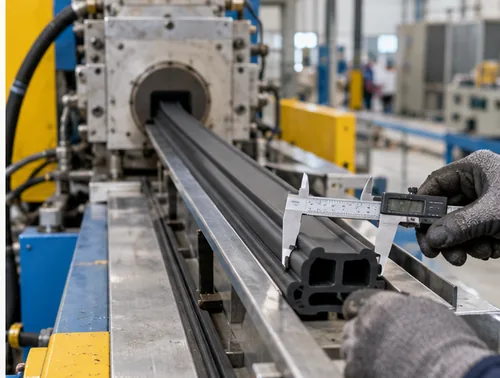
 Rubber Hot Feed Extruder
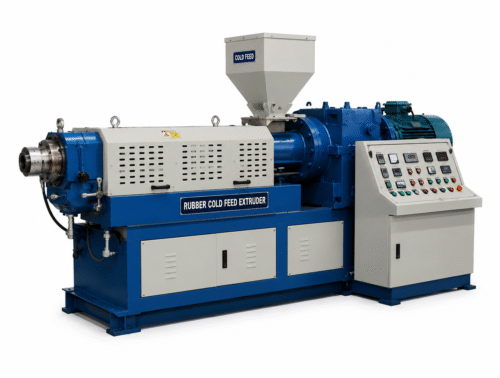 Rubber Cold Feed Extruder
 Rubber Strainer – Reclaim Extruder
 Reclaim Rotary Autoclave
 Compression Molding
 Injection Molding
 Vacuum Molding
 Rubber EVA Refiner Mill
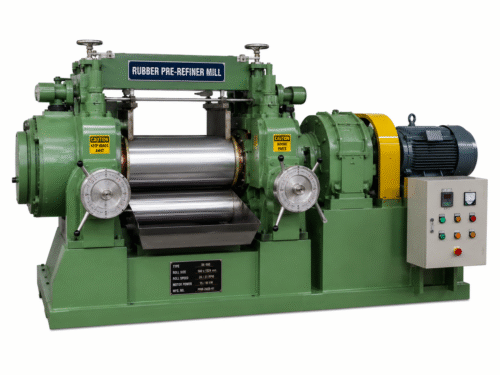 Rubber Pre-Refiner Mill
 Tire Building Machine
 Tread & sidewall Extruder
 Tread Cooling skiver
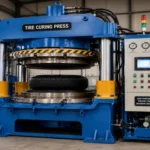 Tire curing press
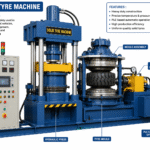
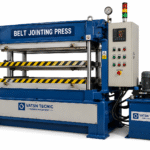 BELT JOINTING PRESS
 Belt Building Machine
 Eva Footwear Injection Molding Machines
 Hawaii Slipper Sole Sheet Machine
 Eva Sole Sheet Splitting
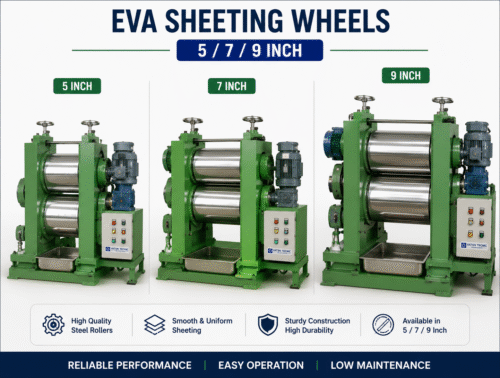 Eva Sheeting Wheels 5/7/9
 PVC Flooring Machine
 Plastic Pelletizing Line
 Filler / Masterbatch / PVC / TPR / EVA
 Breaker – Cracker Mill
 Shredder – Rasper Machines
 Waste Rubber Crumb Grinder Mill
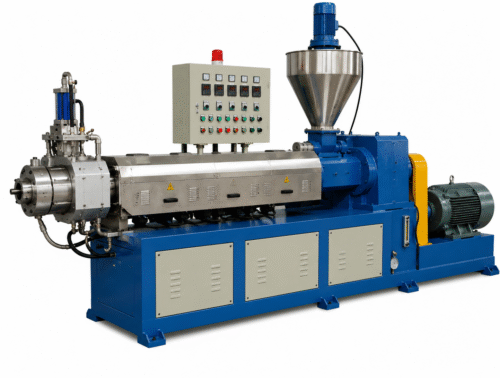
Industrial Rubber Extruder Machine in Kobe: Build a Maintenance Schedule

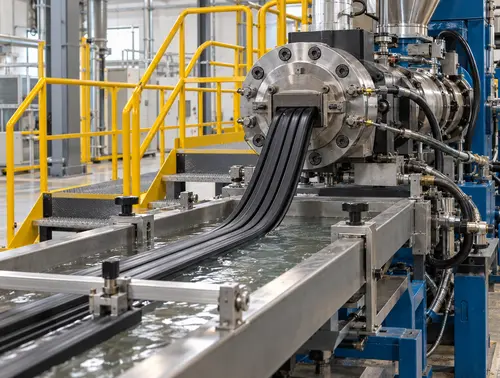
Quick answer: A rubber extruder machine in Kobe will run for years without a maintenance schedule — until the day it stops. The difference between a planned rebuild and an unplanned one is a written schedule built around wear parts, not around breakdowns.
Extruders are forgiving machines, which is exactly why maintenance gets deferred. Buyers taking on a rubber extruder machine in Kobe should ask not only what condition it is in, but what schedule it has been run to, because a machine with no history is a machine with unknown wear.
This guide covers how to build the schedule, what to monitor, and how to decide which spares to hold.
Why schedules fail
Most maintenance schedules fail for one of three reasons: the intervals are copied from a manual that does not match the duty, the checks require dismantling that never happens, or nobody owns the record. The first makes the schedule irrelevant, the second makes it impractical, and the third makes it invisible.
A working schedule is short, specific and owned. Five checks done every week beat twenty checks done never.
Building the schedule around wear parts
Start from the parts that actually wear: the screw, the barrel, the thrust bearing, the gearbox oil, the heaters and the seals. Each has a different failure mode and a different interval.
| Item | Check | Interval guide | Failure if ignored |
|---|---|---|---|
| Screw and barrel | Measure clearance | Annual, or after a contamination event | Output loss, overheating |
| Thrust bearing | Play, noise, oil condition | Quarterly | Sudden seizure |
| Gearbox oil | Level, colour, particles | Monthly, sample annually | Gear wear |
| Heaters | Current draw and setpoint response | Monthly | Zone drift, scrap |
| Screens and seals | Condition, leakage | Each change | Pressure loss, leaks |
The intervals are starting points, not commandments. Adjust them using your own history: if the oil is clean after a year, the interval is too short; if it is dirty after a month, it is too long.
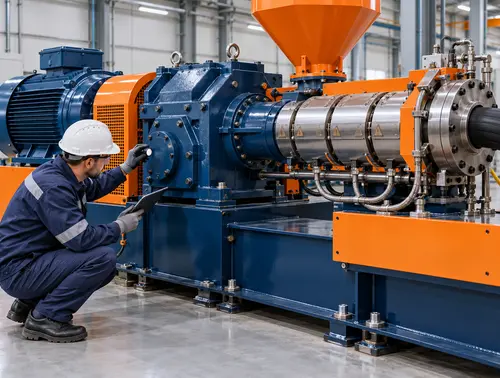
Condition monitoring that actually happens
The checks that get done are the ones that need no dismantling. Temperature readings, oil samples, current logs and noise observations all qualify. A bearing that is starting to fail will show up in temperature or noise before it seizes.
Record the readings, not just the opinion. “Sounds fine” is not a record; “72°C at the thrust bearing, up from 65°C last month” is.
Spares criticality
| Spare | Lead time | Hold? | Reason |
|---|---|---|---|
| Heater bands | Days | Yes, a set | Cheap, stops production |
| Thermocouples | Days | Yes | Failure causes zone drift |
| Thrust bearing | Weeks | Yes if proprietary | Long lead, total stoppage |
| Screw | Months | Only if critical | Expensive, long lead |
| Die | Weeks | Yes for main product | No die, no product |
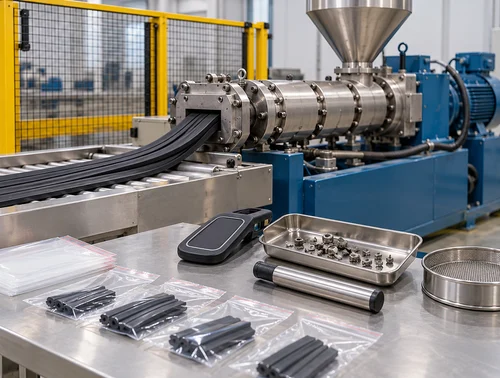
The first year
In the first year, measure more often than you think necessary. You are establishing a baseline, not maintaining a known machine. After twelve months you will know which readings are stable and which drift, and the schedule can be relaxed where the evidence supports it.
Review the schedule annually against the failure history. A schedule that never changes is a schedule nobody is using.
What to ask before buying
Ask for the maintenance records, the oil analysis history and any record of screw or barrel work. If none exist, assume the machine has run to failure and price the first year of inspection accordingly.
Our notes on energy balance and screw geometry explain the two factors that most affect wear rates.
Recording and review
A schedule without a record is a routine, not a system. Record the date, the reading and who took it, in one place the whole team can see. The value comes from the trend, and a trend needs consistent entries.
Review the schedule every quarter against what actually failed. If a check never finds anything, lengthen the interval. If a failure surprised you, add a check that would have caught it earlier.
Keep the record with the machine when it is sold or moved. A documented maintenance history is worth real money on a used extruder, and it costs nothing to keep.
Set a review date in the calendar for the first quarter and keep it. The schedule will be wrong in places, and the only way to correct it is to look at what the records show rather than what the manual predicted.
Keep the review short and change one interval at a time, so you can tell which adjustment made the difference.
Taking on a used extruder? Vatsn Tecnic supplies new, used and refurbished rubber processing machinery. Ask for the maintenance history with the machine, and we will help you build a first-year schedule around what it actually shows.
To read More about Rubber Making Machine Visit Here:
https://www.indiamart.com/vatsntecnic/profile.html
Frequently asked questions
How often should extruder oil be changed?
Follow the manufacturer for the initial interval, then adjust using oil analysis. Sampling tells you more than a fixed calendar.
What is the most critical spare?
The one with the longest lead time that stops production. For many machines that is the thrust bearing or a proprietary die.
Can I predict a bearing failure?
Often, through temperature and noise trends. Vibration analysis adds precision if you have the instrument.
How do I check screw wear without dismantling?
You cannot measure it directly, but falling output and rising stock temperature at constant settings are indicators. Plan a measurement at the next shutdown.
Does the schedule differ for a used machine?
Yes. A used machine needs more frequent checks in the first year because its history is unknown.
What records matter most?
Temperatures, oil samples and any contamination event. These predict most failures.
How long should a screw last?
It depends on the compound and the operating discipline. Abrasive compounds wear screws faster; measure rather than estimate.
Who should own the schedule?
One named person, with a visible record. A schedule shared by everyone is owned by nobody.