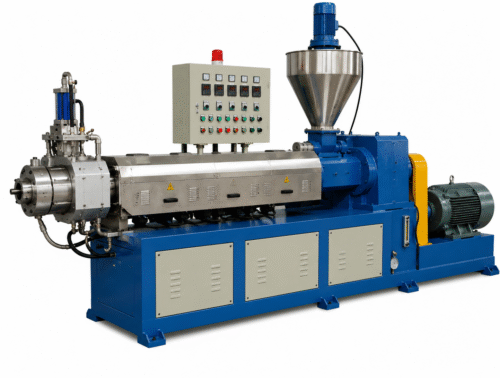
 Rubber Hot Feed Extruder
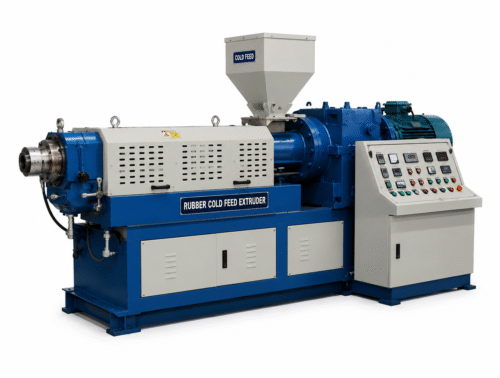 Rubber Cold Feed Extruder
 Rubber Strainer – Reclaim Extruder
 Reclaim Rotary Autoclave
 Compression Molding
 Injection Molding
 Vacuum Molding
 Rubber EVA Refiner Mill
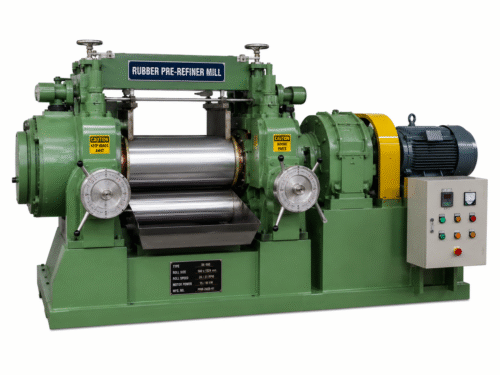 Rubber Pre-Refiner Mill
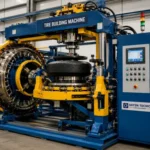 Tire Building Machine
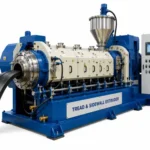 Tread & sidewall Extruder
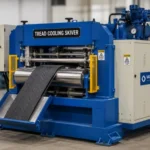 Tread Cooling skiver
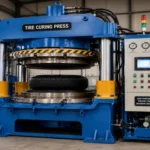 Tire curing press
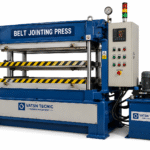 BELT JOINTING PRESS
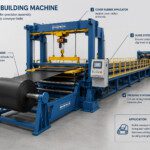 Belt Building Machine
 Eva Footwear Injection Molding Machines
 Hawaii Slipper Sole Sheet Machine
 Eva Sole Sheet Splitting
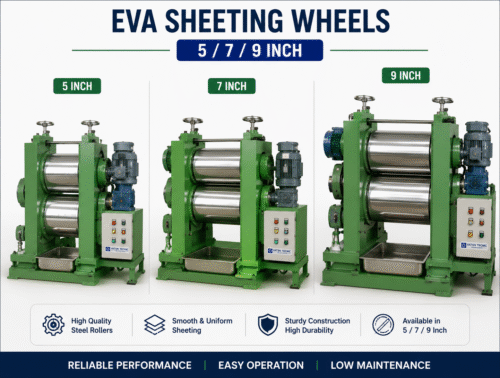 Eva Sheeting Wheels 5/7/9
 PVC Flooring Machine
 Plastic Pelletizing Line
 Filler / Masterbatch / PVC / TPR / EVA
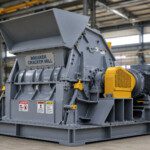 Breaker – Cracker Mill
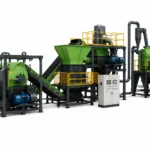 Shredder – Rasper Machines
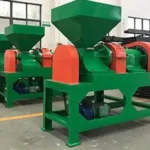 Waste Rubber Crumb Grinder Mill
Buy Rubber Dispersion Kneader in Kolkata: Plan Filler Charging and Dust Control

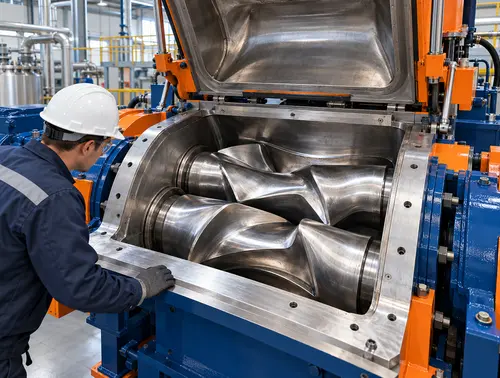
Quick answer: A rubber dispersion kneader in Kolkata lives or dies on how the filler gets in. Carbon black and other powders are light, they drift, and every kilogram that misses the chamber becomes dust in the shed and a variation in the batch.
Kneader performance discussions usually start with rotors and ram pressure. In practice, the charging arrangement decides how repeatable the batch is before the rotors ever touch it. Buyers specifying a rubber dispersion kneader in Kolkata should treat feeding and dust control as part of the machine, not as an afterthought to the layout.
This guide covers what good charging looks like, how dust control interacts with the kneader, and what to settle before the foundation is marked.
Why charging decides batch consistency
A kneader disperses what it is given. If the filler arrives in lumps, or in a different order each cycle, the rotors have to work harder to reach the same dispersion, and the batch temperature rises while they do it. Two batches made from the same recipe can differ simply because the charging sequence differed.
The fix is mechanical rather than procedural: a controlled feed rate, a consistent sequence and a weighing step that does not depend on the operator’s judgement at the end of a shift.
Feeding options and what they change
| Method | Strength | Limitation | Effect on batch |
|---|---|---|---|
| Manual charging | Low cost, flexible | Operator-dependent, dusty | Variable sequence, slower cycles |
| Conveyor with weighing | Repeatable rate and quantity | Needs space and calibration | Consistent fill, shorter cycle |
| Pneumatic conveying | Closed, low dust | Needs dry air and maintenance | Cleanest, but fines can segregate |
Pneumatic systems are the cleanest option and the most demanding. Damp air causes the powder to cake in the line, and fine and coarse fractions can separate on the way to the chamber. If the plant is humid, a conveyor may be the more reliable choice despite the dust.
Dust control at the charging point
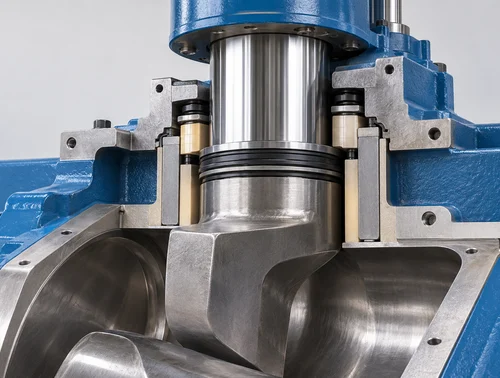
Filler dust is a health and housekeeping problem before it is a quality problem. A local hood over the charging opening, sized for the fill rate rather than the room volume, captures most of it. General ventilation alone moves the dust around.
Check where the hood sits relative to the operator. A hood that pulls air across the operator’s face is uncomfortable and will be disabled within a week. Design the capture away from the working position.
Comparing dust control approaches
| Approach | Strength | Limitation | Best fit |
|---|---|---|---|
| Local hood at the charging point | Captures at source, least dilution | Needs duct routing and fan capacity | Most kneader rooms |
| Enclosed charging station | Best operator protection | Restricts access, needs interlock | High filler loading, tight sheds |
| Room extraction only | Cheap and simple | High background dust, poor capture | Large sheds, low throughput |
Layout for a Kolkata plant
Space is usually tight, and the temptation is to shorten the feed path until the charging station crowds the discharge. That makes both operations slower and dustier. Allow room for a pallet of filler, a weighing station and a walkway that does not cross the discharge zone.
Confirm the floor loading for the filler stack as well as for the kneader. A pallet of carbon black is heavy, and storage is often placed wherever it fits rather than where the slab can carry it.
What to put in the quotation
Ask whether the charging arrangement is in scope, who provides the weighing system, and whether the dust hood is included with the machine or supplied separately. Confirm the fan and ductwork responsibility, and ask for the capture calculation rather than a promise.
Our notes on batch cycle planning and ram seals and guides cover the machine side of the same decisions.
Weighing accuracy and calibration
A weighing system is only as good as its calibration. Check the scale range against your smallest and largest ingredient; a scale sized for a full batch will not resolve a small additive accurately. Confirm the calibration interval and keep a test weight on site.
Record each batch weight rather than only the target. A slow drift in the recorded weights is the earliest sign that a load cell or a feeder is failing, and it is invisible if the operator simply corrects by eye.
Finally, agree who owns the calibration record. In most plants nobody does, and the scale quietly drifts until a batch fails.
Setting up a mixing room? Vatsn Tecnic supplies new, used and refurbished rubber processing machinery. Share your compound and batch size, and ask for the charging and dust-control scope alongside the kneader itself.
To read More about Rubber Making Machine Visit Here:
https://www.indiamart.com/vatsntecnic/profile.html
Frequently asked questions
Does charging method affect dispersion?
Yes. The order and rate at which filler enters the chamber change how the rotors work it and how much heat is generated, which affects dispersion quality.
Is pneumatic conveying worth it?
When the plant is dry and the powder is free-flowing, it is the cleanest option. In humid conditions the line can cake and segregate, so a conveyor may be more reliable.
How do I control dust at the kneader?
Capture it at the charging point with a local hood sized for the fill rate, and keep general ventilation as a secondary measure rather than the primary one.
Can I add weighing later?
Usually yes, if space is left for the equipment. Plan the layout with a weighing station even if you do not buy one immediately.
What causes batch-to-batch variation?
Charging sequence, filler condition, temperature drift and operator judgement. Fixing the charging method removes the largest single source.
Does the dust hood affect cycle time?
Not directly, but a badly placed hood slows the operator and gets disabled. Place it so it does not obstruct the fill.
What about housekeeping?
Filler dust settles on every horizontal surface. A short daily clean is cheaper than the fire and health risks that accumulate when it is ignored.
Should the charging station be enclosed?
For high filler loadings or small sheds, yes. An enclosed station with an interlock gives the best protection, at the cost of access speed.