 Rubber Hot Feed Extruder
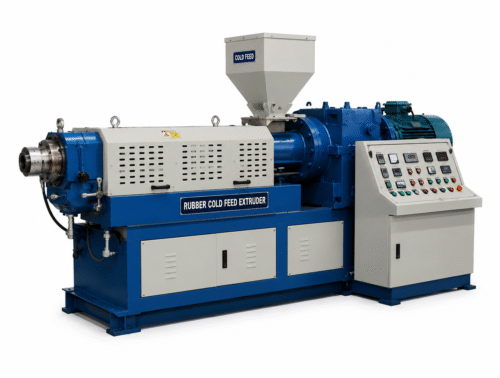 Rubber Cold Feed Extruder
 Rubber Strainer – Reclaim Extruder
 Reclaim Rotary Autoclave
 Compression Molding
 Injection Molding
 Vacuum Molding
 Rubber EVA Refiner Mill
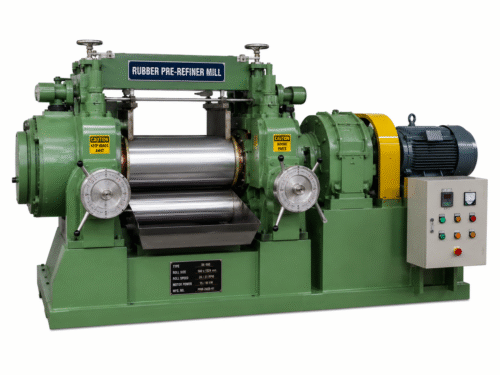 Rubber Pre-Refiner Mill
 Tire Building Machine
 Tread & sidewall Extruder
 Tread Cooling skiver
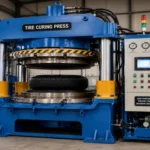 Tire curing press
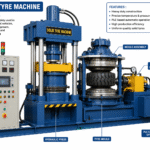
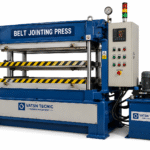 BELT JOINTING PRESS
 Belt Building Machine
 Eva Footwear Injection Molding Machines
 Hawaii Slipper Sole Sheet Machine
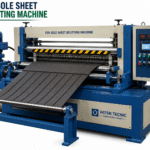 Eva Sole Sheet Splitting
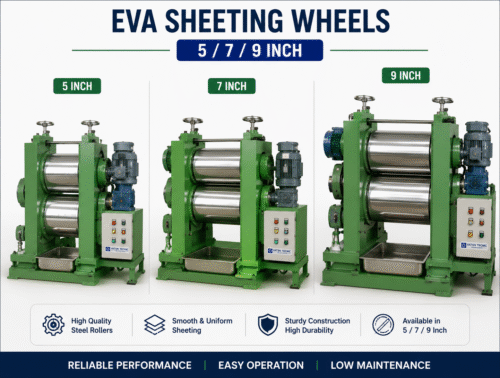 Eva Sheeting Wheels 5/7/9
 PVC Flooring Machine
 Plastic Pelletizing Line
 Filler / Masterbatch / PVC / TPR / EVA
 Breaker – Cracker Mill
 Shredder – Rasper Machines
 Waste Rubber Crumb Grinder Mill
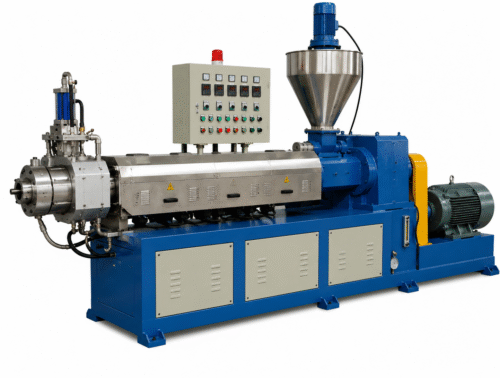
Source Rubber Extruder Machine in Taichung: Match the Screw Geometry

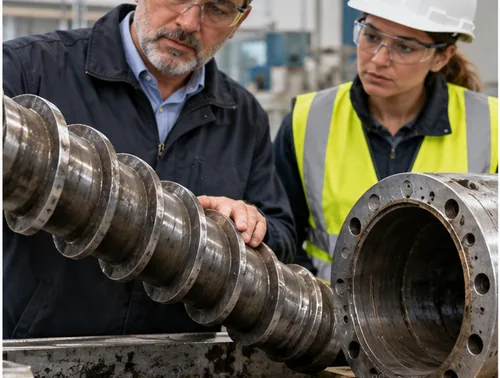
Quick answer: A rubber extruder machine in Taichung should be chosen by screw geometry, not by motor size. The screw’s length-to-diameter ratio and compression decide whether your compound is conveyed gently or worked hard — and that choice is fixed once the screw is made.
Taiwan builds a lot of rubber and plastics machinery, and the used market reflects it: several machines may look identical and behave very differently. For a rubber extruder machine in Taichung, the screw is the specification that matters most and the one sellers describe least precisely.
This guide explains what screw geometry changes, how to read it from the machine, and how to match it to a compound.
What the screw geometry controls
Three numbers describe most of the behaviour: diameter, length-to-diameter ratio and compression ratio. Diameter sets the throughput per revolution. Length-to-diameter ratio sets how much working the compound receives. Compression ratio sets how much the material is squeezed as it travels toward the die.
Length-to-diameter ratio
A longer screw gives more mixing and a more stable output, but it also raises stock temperature and drive load. A shorter screw is gentler and easier to clean, but mixes less. For rubber, moderate ratios are typical because heat is the limiting factor.
Compression ratio
Compression comes from the flight depth changing along the screw. A high compression ratio suits soft compounds that need compacting; a low ratio suits stiff compounds that would otherwise overheat. Using the wrong one shows up as surge, overheating or poor dimensional control.
Reading the screw from the machine
Ask for the screw drawing, not a description. If there is no drawing, measure the flight depth at the feed and at the metering section and note the number of flights. Photograph the screw against a scale. These measurements tell a specialist more than any catalogue.
| Geometry | Effect | Suits | Watch for |
|---|---|---|---|
| Short, low compression | Gentle conveying, low heat | Heat-sensitive compounds | Poor mixing, surge |
| Medium, standard | Balanced | General rubber extrusion | Compromise on extremes |
| Long, high compression | High shear, stable output | Hard, filled compounds | Overheating, high drive load |
Matching geometry to compound and product
Profile extrusion, hose and preforms place different demands on the screw. A profile with thin walls needs stable pressure; a preform needs consistent density. Ask what the machine was previously running and whether the screw was changed for that product.
| Product | Priority | Geometry tendency |
|---|---|---|
| Profile | Dimensional stability | Medium compression, controlled temperature |
| Hose and tube | Surface quality | Gentle compression, good cooling |
| Preform | Density consistency | Higher compression, stable feed |
What else to check on a Taiwanese machine
Confirm the electrical standard, the control panel documentation and the availability of spares. Taiwan-built machines often use standard components, which is an advantage, but confirm the specific drive and controller are supportable locally.
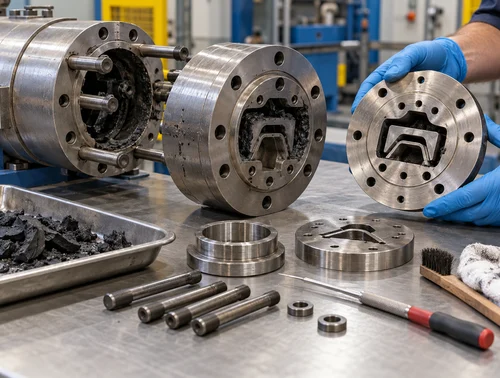
Check the barrel for scoring and the thrust bearing for play. These are the failure points that decide whether the machine runs for years or months. Our notes on screw and barrel wear and filtration screen scope go deeper.
What to put in writing
Record the screw drawing reference, the measured wear figures and the die dimensions in the purchase agreement. A machine described only by model number leaves the most important part of the specification undocumented.
When the geometry is unknown
Older machines often arrive without drawings. In that case, measure what you can: flight depth at the feed and metering sections, pitch, number of flights and the screw length. A specialist can infer the compression ratio from those figures, and that inference is far better than a guess based on the model number.
Photograph the screw with a rule alongside it, at both ends. Those photographs, plus the barrel bore measurements, are the minimum evidence for a sensible decision. If the seller cannot provide them, ask why — a machine that has never been opened for inspection is a machine whose wear is unknown.
Where measurement is impossible, treat the machine as a conveying extruder and plan the die accordingly. That is a conservative assumption, but it is honest, and it protects you from buying a mixing capability that is not there.
If the seller offers a replacement screw, ask who will cut it and to what drawing. A new screw without a specification is not an improvement; it is a second unknown.
Keep that drawing with the machine for as long as you own it; it is the only record of what the screw actually is.
Shortlisting extruders? Vatsn Tecnic supplies new, used and refurbished rubber processing machinery. Send your compound and product details, and ask for the screw geometry before you compare prices.
To read More about Rubber Making Machine Visit Here:
https://www.indiamart.com/vatsntecnic/profile.html
Frequently asked questions
What is L/D ratio?
The screw length divided by its diameter. A higher ratio gives more mixing and more heat; a lower ratio is gentler but mixes less.
Can I change the screw later?
Yes, but a new screw is expensive and must match the barrel and drive. It is better to choose correctly at purchase.
How do I know which geometry suits my compound?
From the compound’s hardness, filler loading and heat sensitivity, plus the product’s tolerance. Ask a screw designer with both details rather than guessing.
Does screw wear change the geometry?
Yes. Wear reduces flight depth and increases clearance, which lowers compression and output. Measured wear figures matter more than the original drawing alone.
What causes surge?
Often a feed or compression mismatch, or worn flights. Check the screw measurements and the feed arrangement before blaming the die.
Are Taiwanese machines easy to support?
Generally, because many use standard components. Confirm the specific drive and controller can be serviced locally.
What should I check on the barrel?
Scoring, straightness and the liner condition if lined. A scored barrel cannot be fixed by a new screw.
How do I verify the machine before shipping?
Ask for a run with a representative compound, screw measurements and photographs of the die and barrel. If a trial is impossible, at least obtain the drawing.