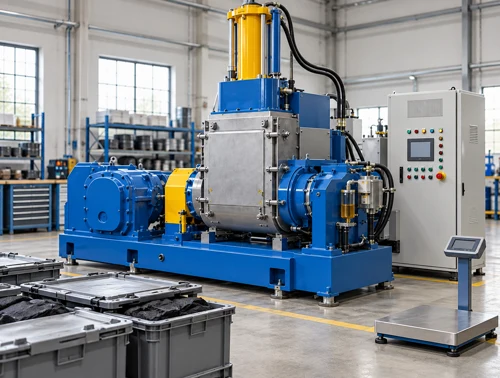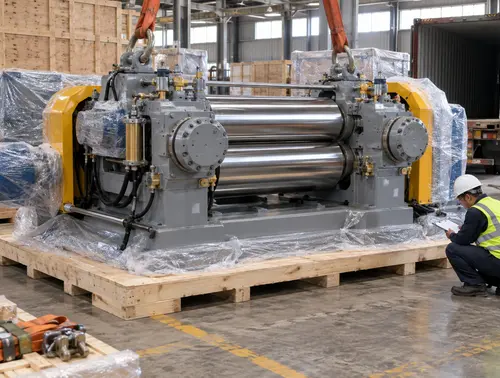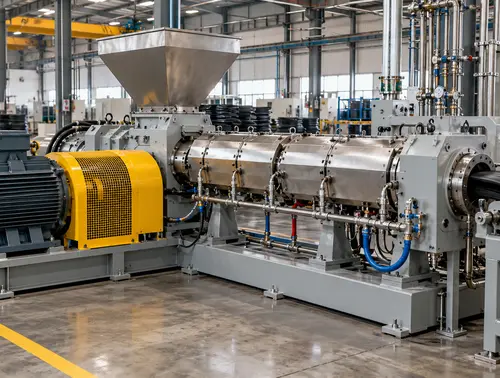
 Rubber Hot Feed Extruder
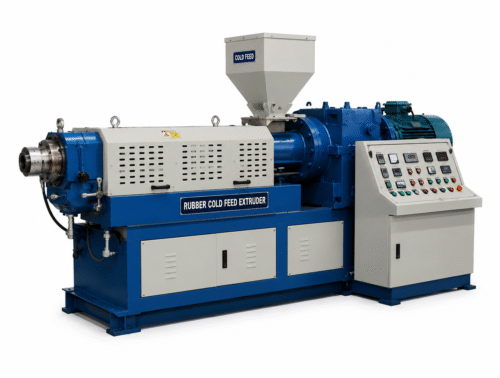 Rubber Cold Feed Extruder
 Rubber Strainer – Reclaim Extruder
 Reclaim Rotary Autoclave
 Compression Molding
 Injection Molding
 Vacuum Molding
 Rubber EVA Refiner Mill
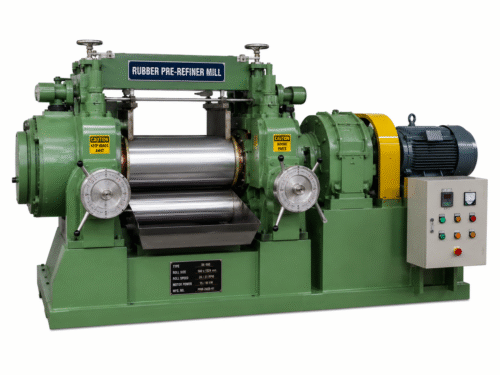 Rubber Pre-Refiner Mill
 Tire Building Machine
 Tread & sidewall Extruder
 Tread Cooling skiver
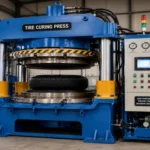 Tire curing press
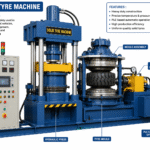
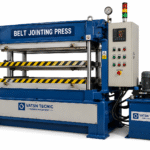 BELT JOINTING PRESS
 Belt Building Machine
 Eva Footwear Injection Molding Machines
 Hawaii Slipper Sole Sheet Machine
 Eva Sole Sheet Splitting
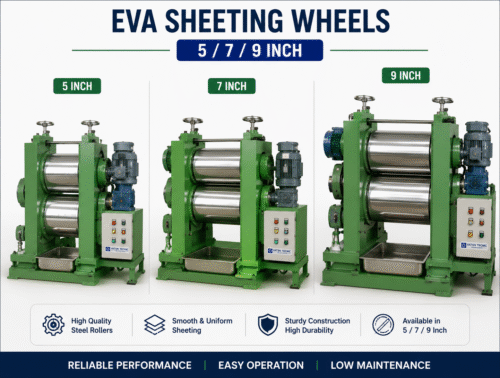 Eva Sheeting Wheels 5/7/9
 PVC Flooring Machine
 Plastic Pelletizing Line
 Filler / Masterbatch / PVC / TPR / EVA
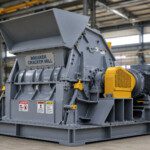 Breaker – Cracker Mill
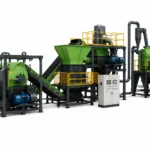 Shredder – Rasper Machines
 Waste Rubber Crumb Grinder Mill
Source Rubber Calendar Machine in Ahmedabad: Match Web Handling and Winding

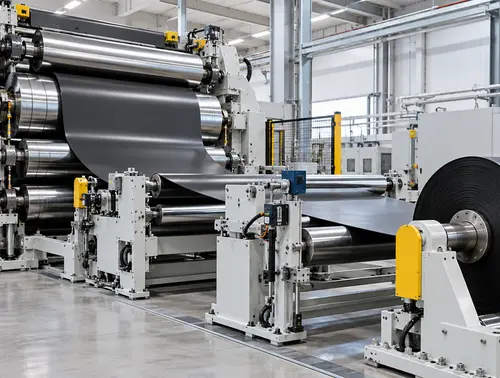
When you source a rubber calendar machine in Ahmedabad, match the rolls to the entire web path. A suitable calender can still disappoint if guides, cooling, tension control, edge alignment, liner handling and winding are missing or incompatible. Define the incoming material, finished sheet, roll format and downstream task before comparing quotations.
Describe the product, not just the machine
Give suppliers the target application, material family, width range, thickness or coating objective, liner requirement and expected roll-handling method. Treat all values as project inputs to be confirmed rather than generic machine capabilities. If several products will run, identify a representative trial for each materially different web-handling case.
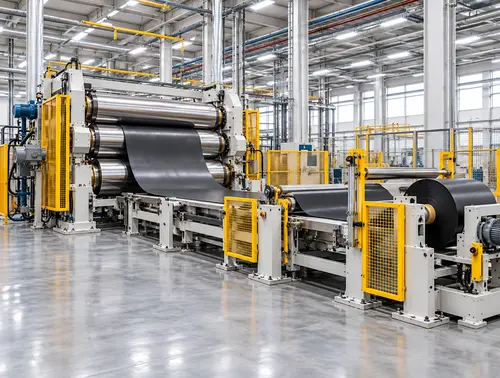
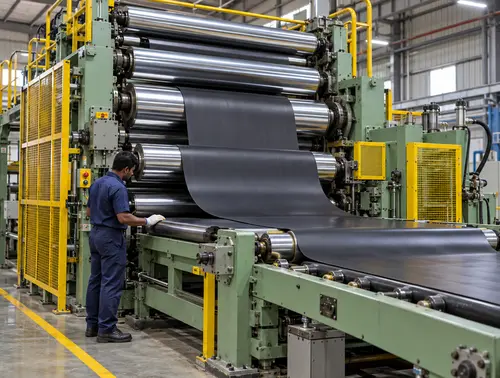
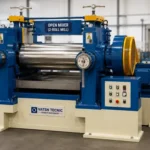
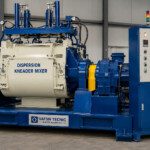
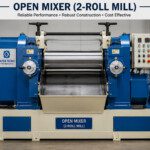
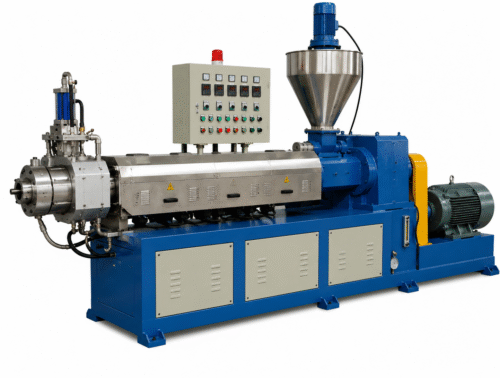
The images are illustrative and do not demonstrate the condition or availability of a specific line. For roll-focused due diligence, also review Vatsn Tecnic’s used rubber calender roll inspection guide.
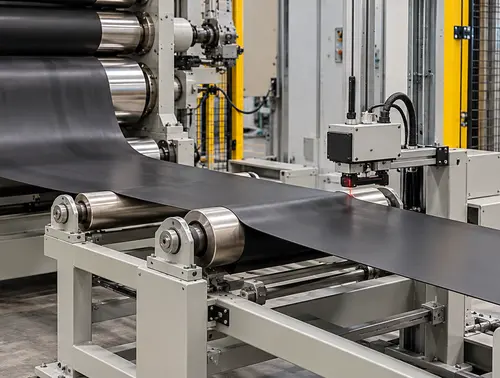
Draw the web path end to end
Create one drawing from feed preparation through the roll stack to cooling, guiding, inspection, liner application, slitting if required and winding. Mark the web direction, access side, roll changes and operator stations. A verbal scope often hides a missing transition roller, unsuitable winding position or conflict with building columns.
| Section | Decision to document | Risk if omitted |
|---|---|---|
| Infeed | Material form, centring and tension method | Unstable entry into the nip |
| Calender rolls | Configuration, surface condition and process objective | Machine selected without a representative trial |
| Cooling and guiding | Required path, adjustment and edge reference | Sheet wanders or is wound before it is suitable |
| Winder | Core, liner, roll weight and handling method | Finished rolls cannot be changed safely or consistently |
Separate web quality from roll quality
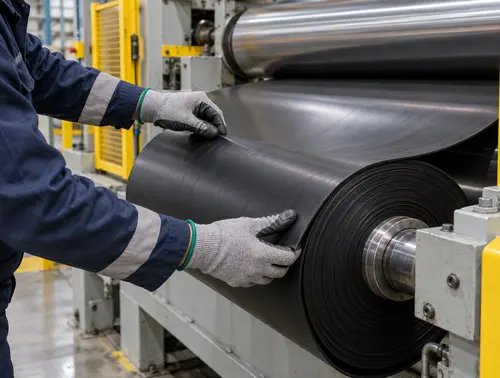
A visually good sheet at the calender exit does not prove that the finished roll will be usable. Observe tracking, wrinkles, edge position, liner laydown, telescoping and roll change. Agree where width and thickness are measured and how samples are identified. Record speed and process conditions so results can be compared fairly.
Machine guarding and safe access must be addressed for every nip and winding point. The US OSHA machine-guarding resource is useful general background, while the applicable local rules, risk assessment and manufacturer instructions control the actual installation.
| Winding choice | Advantage | Trade-off |
|---|---|---|
| Simple driven winder | Lower complexity for a narrow, proven duty | May offer limited control across changing roll diameter |
| Closed-loop tension control | Can support more consistent winding when correctly integrated | Adds sensors, tuning and maintenance requirements |
| Manual edge adjustment | Simple and visible to operators | Depends heavily on attention and access |
| Automatic edge guiding | Can correct lateral drift within its designed range | Needs suitable sensor reference, actuator and web path |
Build a complete quotation scope
When you source a rubber calendar machine in Ahmedabad, list every included stand, roller, drive, sensor, guard, platform, control panel, cable, cooling connection and handling aid. Identify exclusions beside the corresponding interface. Ask whether installation drawings, control narratives, spare-parts lists, training and trial support are included.
Do not accept a line speed, output or tolerance claim without its conditions. Ask what material, width, thickness, test length and measurement method support the statement. If your product differs, arrange a representative trial or treat the claim as unverified.
Witness-test checklist
- Confirm machine and component identities.
- Review the full web-path drawing against the offered scope.
- Inspect guarding, access and isolation with competent personnel.
- Thread the representative material using the planned method.
- Record process settings and measurement locations.
- Observe guiding, cooling, liner and winding behaviour.
- Inspect the finished roll after the agreed length.
- Document defects, owners and closure dates.
Plan utilities, access and future products
Web-handling equipment occupies more floor space than the roll stack alone. Mark operator aisles, roll-change zones, lifting routes, electrical panels, cooling connections and safe maintenance access on the site layout. Check doorways and transport paths before dispatch. If the line will be installed in stages, define temporary guards and controls rather than assuming the final arrangement will be available from day one.
Discuss future products without turning the purchase into an unsupported “universal” specification. Identify which change parts, roller positions, sensor ranges or control recipes would be needed for a wider material or width range. Ask the supplier to separate proven capability, capability requiring a new trial and capability that is only a design possibility.
Information to preserve after commissioning
Keep the approved web-path drawing, roller and sensor settings, trial run sheets, labelled samples, finished-roll photographs and open-item closure records together. This baseline helps maintenance teams distinguish later drift from the original accepted condition. It also gives production teams a controlled starting point without implying that one recipe suits every compound.
To read More about Rubber Making Machine Visit Here:
https://www.indiamart.com/vatsntecnic/profile.html
Frequently asked questions
Is the winder normally included with a calender?
Do not assume it. The quotation and layout must state the exact downstream equipment and interfaces.
Why does the liner matter?
It can affect release, roll build and handling. Define its material, width, feed and take-up method for the intended product.
Can edge guiding fix every tracking problem?
No. Misalignment, uneven tension, unsuitable rollers or material variation may require correction elsewhere in the path.
What should a representative trial include?
Use an agreed material and run enough length to observe steady operation, guiding and winding rather than only a short sample.
Should thickness be checked at one point?
A single point can miss cross-width variation. Agree the measurement pattern and instrument before the trial.
How are finished rolls handled?
Define core, expected roll size, unloading method, lifting aids and storage route as part of the line scope.
What documents should be supplied?
Request layout, utilities, electrical information, control narrative, manuals, parts list, drawings and trial record.
Does a clean sample prove production performance?
No. A sample is evidence only for the recorded material, settings, length and inspection method.
Next step
Send Vatsn Tecnic your product and roll-handling requirements. Ask for an end-to-end scope drawing before you source a rubber calendar machine in Ahmedabad.